
gable box die
Showing the single result
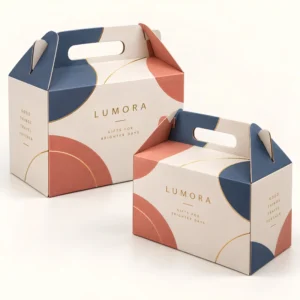
A gable box die is the shaped cutting tool that stamps out the flat blank for a gable box, cutting its outline, cutting the handle opening and creasing the fold lines in one precise operation. Without an accurate die, even beautiful artwork can fail in production, because panels will not align, the handle will not lock and the box will not fold cleanly. Understanding how a gable box die works helps buyers brief a job correctly, check artwork against the die line and avoid delays.
What a gable box die does in production
In carton production, a die is a flat board or a cylinder fitted with steel cutting rules and creasing rules, arranged to match the exact shape of the unfolded box. The board is fed through, the cutting rules slice the outline and any windows or handle slots, and the creasing rules press fold lines into the board without cutting through it. The finished blank is then printed, folded and glued into the familiar peaked shape with a handle. Because the die controls every edge and fold, a small error in the die line can affect the whole run, which is why die lines are checked so carefully before production. For context on the finished shape, see the gable box collection and note how the peaked top and handle relate to the flat blank.
Dies are made for a specific box size and structure, not for all gable boxes in general. Changing the length, width, height, handle shape or window position usually means a new or modified die, because each of those features is defined by the position of a rule. That is one reason custom sizes need careful planning: the die is part of the setup, and getting it right once makes every repeat run more reliable. Keep the approved die line with your product specification, so reorders use the same shape and fold positions.
Parts of a gable box die line
A die line drawing shows the unfolded box as a flat layout, with different line types for cuts, folds and glue areas. Cut lines show where the board will be sliced, including the outer outline, the handle opening and any window aperture. Crease lines show where the board will fold, including the base folds, side folds and the angled folds that form the peaked top. Glue tabs and lock tabs are also marked, so artwork and assembly instructions can be planned around them. If you receive a die line template for artwork, use that exact file, do not redraw the shape from a photograph or a finished box, because even a small redraw error can shift print across a fold.
Cut lines, crease lines and safe areas
Cut lines define the final edge, crease lines define the fold, and the safe area is the zone inside the cut line where essential text and logos should sit. Keep logos, names and important details well inside the safe area, so a tiny shift during cutting or folding does not clip them. Extend background colours and patterns beyond the cut line into the bleed area where requested, so the printed colour reaches the edge without a white fringe. Ask which line colours represent cuts, creases and bleed in your template, because conventions can vary between suppliers.
Die cutting, creasing and board behaviour
Different boards behave differently under a die. Thin folding board cuts cleanly and folds crisply, but can tear if a handle slot is too narrow or a fold is too sharp. Thicker corrugated board needs stronger creasing and wider fold allowances, and its fluted structure can affect how precisely a small handle opening cuts. Grain direction matters too: board folds more cleanly along the grain than across it, so the die layout should respect grain where possible. A good production check includes folding a sample blank by hand, checking that creases do not crack the print and that the handle locks without forcing.
Common die related problems
Common problems include a handle that tears at the slot, a base that will not lock flat, a lid that sits unevenly, and print that lands across a fold where it was meant to sit on a flat panel. Most of these trace back to artwork placed without reference to the die line, or to a board that is too thick or too thin for the die as set. Catching them at sample stage is straightforward: fold the sample, fill it, carry it and inspect every panel, rather than judging the box only as a flat printed sheet.
Artwork setup for a gable box die
Setting artwork to a gable box die starts with placing your design on the supplied template at actual size, with layers or guides kept intact until the file is approved. Align panels to the die line, keep text out of glue tabs and handle slots, and avoid placing a face, a logo or a key word across a crease where the fold will distort it. Supply the file in the format requested, at high resolution, with fonts embedded or outlined as instructed, and include a clear note about colours and finishes. A tidy artwork file reduces questions, speeds approval and lowers the risk of a production hold.
Checking a die line proof
A die line proof is your chance to confirm shape before cutting steel or committing to a full run. Check the overall dimensions against your product measurements, check the handle width against a comfortable grip, and check that the base size matches the tray or insert you plan to use. Fold a printed proof if one is available, or fold a plain sample blank, and test it with the real product inside. Confirm window positions, lock tabs and glue areas, and sign off only when the folded shape, not just the flat drawing, meets your brief.
What to record for repeat orders
Record the die reference, the finished box dimensions, the board type and thickness, the handle style and any window size, alongside your artwork version. That record lets a repeat order reuse the same tooling and the same layout, which keeps quality consistent and avoids a fresh setup discussion each time. If you change the product, even slightly, revisit the die record first, because a taller jar or a wider tray may need a size change that affects the die.
Ordering boxes made with a gable box die
When you enquire, share the finished size you need, the product it will hold, the board preference and whether you already have a die line or need one created. Standard boxes are usually produced in 10 to 14 working days after final artwork approval, corrugated boxes take 12 to 15 working days after final artwork approval, and rigid or specialist constructions take 13 to 16 working days after final artwork approval. These timings cover production after approval, not a guaranteed delivery date, and die creation or modification should be allowed for in your schedule where it applies. To discuss a size or a die line for your product, request a quote for gable box production and include your dimensions and artwork status.
Frequently asked questions
What is a gable box die?
A gable box die is the cutting tool that shapes the flat blank for a gable box, cutting its outline and handle opening and creasing its fold lines. It defines the finished size and shape of the box.
Do I need a new die for a different gable box size?
Yes, in most cases a different size, handle shape or window position needs a new or modified die, because the die line defines each of those features. Keep the approved die line on record for repeat orders at the same size.
Can I place artwork anywhere on a gable box die line?
No, artwork should respect cut lines, crease lines, glue tabs and safe areas shown on the die line template. Keep essential text on flat panels and away from folds, handle slots and glue areas.
How do I check a gable box die line before production?
Check dimensions against your product, fold a sample blank, fill it with the real product and test the handle and base. Approve the shape only after the folded box, not just the flat drawing, meets your brief.